
Por que isso é difícil?
Pre-assembly pays off through labour removed from site, and the mechanisms that limit it are physical rather than financial.
- Site labour cost per hour is typically several times factory labour cost, so labour transferred to the factory carries a multiplied saving
- Field assembly happens in weather, at height and often under schedule pressure, all of which reduce productivity and increase rework
- Transport volume and weight limits cap the pre-assembly level, since a larger sub-assembly packs less densely
- Lifting capacity on site constrains unit weight, and a sub-assembly that cannot be lifted by available equipment is not pre-assembled in any useful sense
- Tolerance accumulation is reduced by factory assembly, because jig-based work holds dimensions that site work cannot
- The optimum differs by market, since it depends entirely on the ratio of factory to field labour cost in the destination country
Requisitos de engenharia
These are the inputs that determine the right pre-assembly level.
- Site labour rate and expected productivity for each assembly operation, so the value of removing site work can be calculated
- Transport mode and container dimensions, with the maximum unit size and weight that can be shipped
- On-site lifting equipment available, and the maximum unit weight it can handle
- Assembly sequence and the structure of the work fronts, since pre-assembly should match how the site actually builds
- Tolerance requirements at each interface, since factory assembly is most valuable where tolerances accumulate
- Site conditions, including weather exposure, access and the availability of a secure staging area
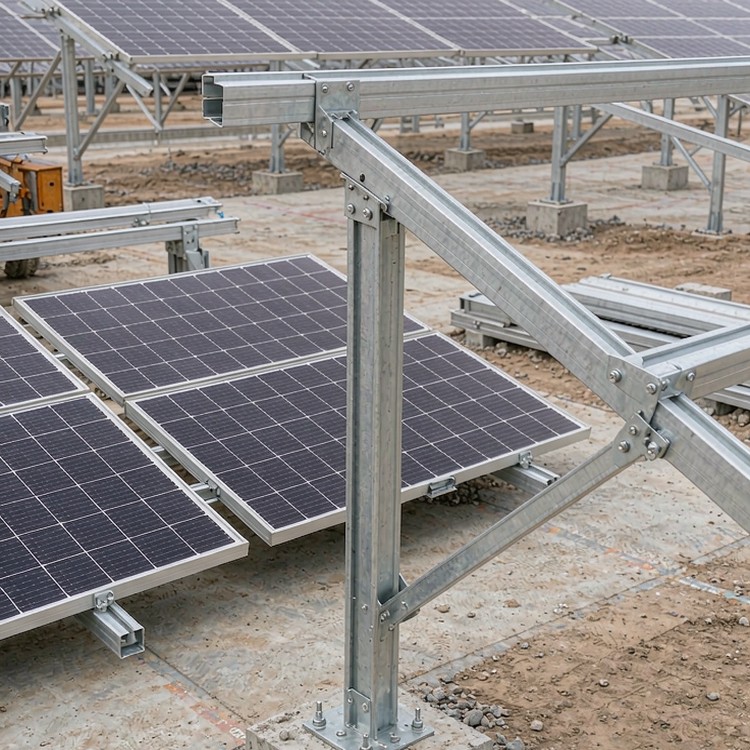
Selection guidance: compare factory and field labour cost per hour before deciding the level. The right answer varies by market, and a level chosen without that ratio is a preference rather than a decision.
Como resolvemos isso
- Sub-assembly units designed to the largest size that transport and site lifting allow, capturing the maximum labour transfer within the physical limits
- Factory jig assembly for the interfaces where tolerances accumulate, so site work begins from an accurate starting geometry
- Kits labelled and packaged by installation sequence, so crews assemble rather than search
- Bolt and fastener lots supplied matched to each sub-assembly, eliminating site sorting and reducing the risk of incorrect fasteners
- Touch-up and joint detailing designed for factory completion, so the fewest possible operations remain for the field
- Installation manual stating the pre-assembly level, the equipment needed and the expected daily output per crew
Além da estrutura
- Pre-assembly plan reviewed against the construction programme, since the level also sets how much staging area the site needs
- Support during the first work fronts, where a supervisor trains the crew on the assembly sequence before it becomes routine
Benchmarks de referência
Os benchmarks abaixo são projetos de referência da indústria, de tipo e escala comparáveis e documentados publicamente, citados para ilustrar a prática de engenharia. Eles não representam nosso histórico de entregas.
- A 200 MW project in Australia where sub-assemblies were sized to the maximum container dimensions, transferring a substantial share of field bolting to the factory.
- A 150 MW project in Chile where site lifting capacity, not container volume, set the pre-assembly ceiling and the design was adjusted accordingly.
- A 250 MW programme in the Middle East where tolerance-critical interfaces were factory jig-assembled, reducing rework during the first weeks of installation.
Normas e Conformidade
- ASCE 7 / EN 1991 cargas de vento resolvidas com fatores de terreno e exposição específicos do local
- Compatibilidade da interface do módulo IEC 61215 / IEC 61730 verificada em relação à folha de dados do seu módulo.
- Classes de execução EN 1090 ou AISC para estruturas de aço soldadas e aparafusadas
- Galvanização a quente conforme ISO 1461, massa de zinco especificada pela corrosividade do solo e da atmosfera.
- Gestão da qualidade da produção segundo a norma ISO 9001 com rastreabilidade ao nível do lote.
- Pacote de documentação CE/EN 1090, quando exigido pelos mercados de destino.
Garantia de Qualidade
O controle de qualidade é baseado em pontos de verificação: verificação da entrada de materiais, inspeção da posição de soldas e furos durante o processo, amostragem da espessura do revestimento e revisão do contêiner antes do embarque. Cada ponto de verificação gera um documento que sua equipe de qualidade pode arquivar, e a inspeção pré-embarque pode ser realizada pelo seu inspetor ou por uma empresa terceirizada.
Documentação que você receberá
A documentação é tão importante quanto o aço. A cada entrega, você recebe certificados de testes de fábrica rastreáveis por lote; registros de galvanização por lote, de acordo com a norma ISO 1461 ou a norma especificada por você; relatórios de inspeção dimensional de gabaritos de pré-montagem; rastreabilidade de lotes de parafusos e ferragens; desenhos "como construído" com as adaptações necessárias no local; e um documento de garantia que especifica os casos de carga cobertos, a vida útil de projeto e os procedimentos para reclamações. Tudo é indexado, portanto, seu registro de ativos não depende da memória de um único engenheiro.
Planejamento de Vida Útil e Manutenção
A vida útil é um resultado do projeto, não uma promessa. A massa de zinco, a classe de revestimento dos fixadores, os detalhes da drenagem e o isolamento de metais diferentes são selecionados de acordo com a categoria de corrosividade do seu local, e o intervalo esperado para a primeira manutenção é especificado por escrito. Para ambientes agressivos, reforçamos o sistema de revestimento na fase de projeto, o que é sempre mais econômico do que uma adaptação posterior.
Custos e considerações comerciais
- Pre-assembly reduces site labour hours, and the value of the reduction depends on the local labour rate rather than on the quantity of work moved
- Freight volume rises with the pre-assembly level, so the trade is between container count and site labour hours
- Staging area requirements change with unit size, and a larger staging footprint may itself be a cost on constrained sites
- Tolerance-critical factory assembly reduces rework, which is a cost that rarely appears in a quotation and frequently appears in a construction budget
- Installation productivity improvement is the most measurable outcome, and it should be stated as daily output per crew rather than as a percentage claim
Perguntas frequentes
How much pre-assembly is worth doing?
Does pre-assembly reduce quality risk?
What limits how far we can go?
How is the pre-assembly level decided?
Does pre-assembly change the site programme?
Guias e páginas de aplicativos relacionados
Continue com as páginas mais próximas do seu tipo de projeto.
- Logistics, Pre-Assembly & Installation – a visão geral do grupo para esta escala
- Eficiência no carregamento e transporte de contêineres
- Produtividade e cronograma de construção da cravação de estacas
- Montagem flexível e aplicações de grande vão
- Mountain & Steep-Terrain Solar Projects
- Projetos de energia solar para o mercado regional
O que precisamos para cotar
- Site labour rates and expected productivity for installation operations
- Transport mode, container dimensions and any over-dimensional cargo allowance
- Lifting equipment available on site, with its capacity
- Construction programme and the number of work fronts expected
Fale com um engenheiro estrutural.
Send the site labour rates, transport constraints and programme, and we will return a recommended pre-assembly level per component family with the freight and labour effects quantified.
 English
 Español
 Deutsch
 Português
 Français
 Italiano
