
Perché questo è difficile
Pre-assembly pays off through labour removed from site, and the mechanisms that limit it are physical rather than financial.
- Site labour cost per hour is typically several times factory labour cost, so labour transferred to the factory carries a multiplied saving
- Field assembly happens in weather, at height and often under schedule pressure, all of which reduce productivity and increase rework
- Transport volume and weight limits cap the pre-assembly level, since a larger sub-assembly packs less densely
- Lifting capacity on site constrains unit weight, and a sub-assembly that cannot be lifted by available equipment is not pre-assembled in any useful sense
- Tolerance accumulation is reduced by factory assembly, because jig-based work holds dimensions that site work cannot
- The optimum differs by market, since it depends entirely on the ratio of factory to field labour cost in the destination country
Requisiti di ingegneria
These are the inputs that determine the right pre-assembly level.
- Site labour rate and expected productivity for each assembly operation, so the value of removing site work can be calculated
- Transport mode and container dimensions, with the maximum unit size and weight that can be shipped
- On-site lifting equipment available, and the maximum unit weight it can handle
- Assembly sequence and the structure of the work fronts, since pre-assembly should match how the site actually builds
- Tolerance requirements at each interface, since factory assembly is most valuable where tolerances accumulate
- Site conditions, including weather exposure, access and the availability of a secure staging area
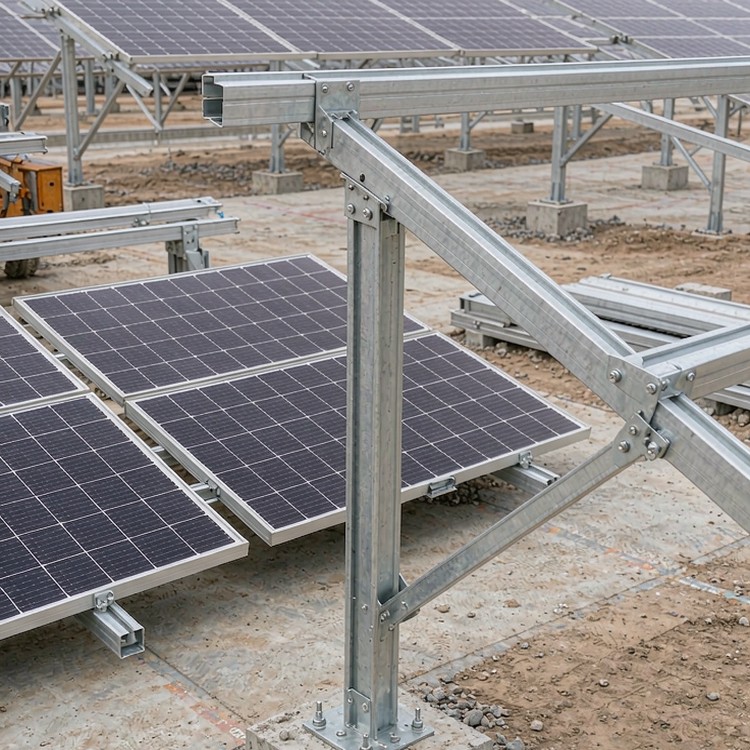
Selection guidance: compare factory and field labour cost per hour before deciding the level. The right answer varies by market, and a level chosen without that ratio is a preference rather than a decision.
Come lo risolviamo
- Sub-assembly units designed to the largest size that transport and site lifting allow, capturing the maximum labour transfer within the physical limits
- Factory jig assembly for the interfaces where tolerances accumulate, so site work begins from an accurate starting geometry
- Kits labelled and packaged by installation sequence, so crews assemble rather than search
- Bolt and fastener lots supplied matched to each sub-assembly, eliminating site sorting and reducing the risk of incorrect fasteners
- Touch-up and joint detailing designed for factory completion, so the fewest possible operations remain for the field
- Installation manual stating the pre-assembly level, the equipment needed and the expected daily output per crew
Oltre la struttura
- Pre-assembly plan reviewed against the construction programme, since the level also sets how much staging area the site needs
- Support during the first work fronts, where a supervisor trains the crew on the assembly sequence before it becomes routine
Parametri di riferimento
I parametri di riferimento riportati di seguito sono progetti di settore di tipo e dimensioni comparabili, documentati pubblicamente e citati a scopo illustrativo delle migliori pratiche ingegneristiche. Non rappresentano il nostro storico di realizzazione.
- A 200 MW project in Australia where sub-assemblies were sized to the maximum container dimensions, transferring a substantial share of field bolting to the factory.
- A 150 MW project in Chile where site lifting capacity, not container volume, set the pre-assembly ceiling and the design was adjusted accordingly.
- A 250 MW programme in the Middle East where tolerance-critical interfaces were factory jig-assembled, reducing rework during the first weeks of installation.
Standard e conformità
- Carichi del vento ASCE 7 / EN 1991 risolti con fattori di terreno ed esposizione specifici del sito
- Compatibilità dell'interfaccia del modulo IEC 61215 / IEC 61730 verificata rispetto alla scheda tecnica del modulo.
- Classi di esecuzione EN 1090 o AISC per carpenteria metallica saldata e bullonata
- Zincatura a caldo secondo ISO 1461, massa di zinco specificata in base alla corrosività del suolo e dell'atmosfera.
- Gestione della qualità della produzione secondo la norma ISO 9001 con tracciabilità a livello di lotto.
- Documentazione CE/EN 1090 ove richiesta dai mercati di destinazione.
Garanzia di qualità
Il controllo qualità si basa su punti di controllo: verifica dell'ingresso del materiale, ispezione in corso di saldatura e posizione dei fori, campionamento dello spessore del rivestimento e controllo del contenitore prima della spedizione. Ogni punto di controllo genera un documento che il vostro team di controllo qualità può archiviare, e l'ispezione pre-spedizione è a disposizione del vostro ispettore o di una terza parte.
Documentazione che riceverai
La documentazione è importante quanto l'acciaio stesso. Per ogni consegna riceverete certificati di collaudo del laminatoio riconducibili ai numeri di lotto; registri di zincatura per lotto conformi alla norma ISO 1461 o allo standard da voi specificato; rapporti di ispezione dimensionale delle dime di preassemblaggio; tracciabilità dei lotti di bulloni e componenti; disegni as-built laddove siano state apportate modifiche in cantiere; e un documento di garanzia che specifica i casi di carico coperti, la durata di vita utile prevista e le procedure di reclamo. Tutto è indicizzato, in modo che il registro delle risorse non dipenda dalla memoria di un singolo ingegnere.
Pianificazione della durata di servizio e della manutenzione
La durata di servizio è un risultato di progettazione, non una promessa. La massa di zinco, la classe di rivestimento dei dispositivi di fissaggio, i dettagli di drenaggio e l'isolamento tra metalli diversi vengono selezionati in base alla categoria di corrosività del sito e l'intervallo previsto per la prima manutenzione viene indicato per iscritto. Per ambienti aggressivi, in fase di progettazione, il sistema di rivestimento viene potenziato, il che è sempre più economico di un intervento successivo.
Considerazioni di costo e commerciali
- Pre-assembly reduces site labour hours, and the value of the reduction depends on the local labour rate rather than on the quantity of work moved
- Freight volume rises with the pre-assembly level, so the trade is between container count and site labour hours
- Staging area requirements change with unit size, and a larger staging footprint may itself be a cost on constrained sites
- Tolerance-critical factory assembly reduces rework, which is a cost that rarely appears in a quotation and frequently appears in a construction budget
- Installation productivity improvement is the most measurable outcome, and it should be stated as daily output per crew rather than as a percentage claim
Domande frequenti
How much pre-assembly is worth doing?
Does pre-assembly reduce quality risk?
What limits how far we can go?
How is the pre-assembly level decided?
Does pre-assembly change the site programme?
Guide correlate e pagine applicative
Proseguite con le pagine più pertinenti alla tipologia del vostro progetto.
- Logistica, preassemblaggio e installazione – la panoramica del gruppo per questa fascia di scala
- Efficienza nel carico e nella spedizione dei container
- Produttività e programma di costruzione per la posa dei pali
- Montaggio flessibile e applicazioni a lunga campata
- Progetti solari in montagna e su terreni scoscesi
- Progetti solari per il mercato regionale
Cosa dobbiamo preventivare
- Site labour rates and expected productivity for installation operations
- Transport mode, container dimensions and any over-dimensional cargo allowance
- Lifting equipment available on site, with its capacity
- Construction programme and the number of work fronts expected
Rivolgiti a un ingegnere strutturale.
Send the site labour rates, transport constraints and programme, and we will return a recommended pre-assembly level per component family with the freight and labour effects quantified.
 English
 Español
 Deutsch
 Português
 Français
 Italiano
